Multi-Level Carton Flow Racks
Stacked 3-to-6-tier carton flow rack systems that multiply pick face density in the same floor footprint — more SKUs per aisle foot, more picks per operator travel step. Engineered for high-SKU distribution, assembly line feeding, and pick module integration.
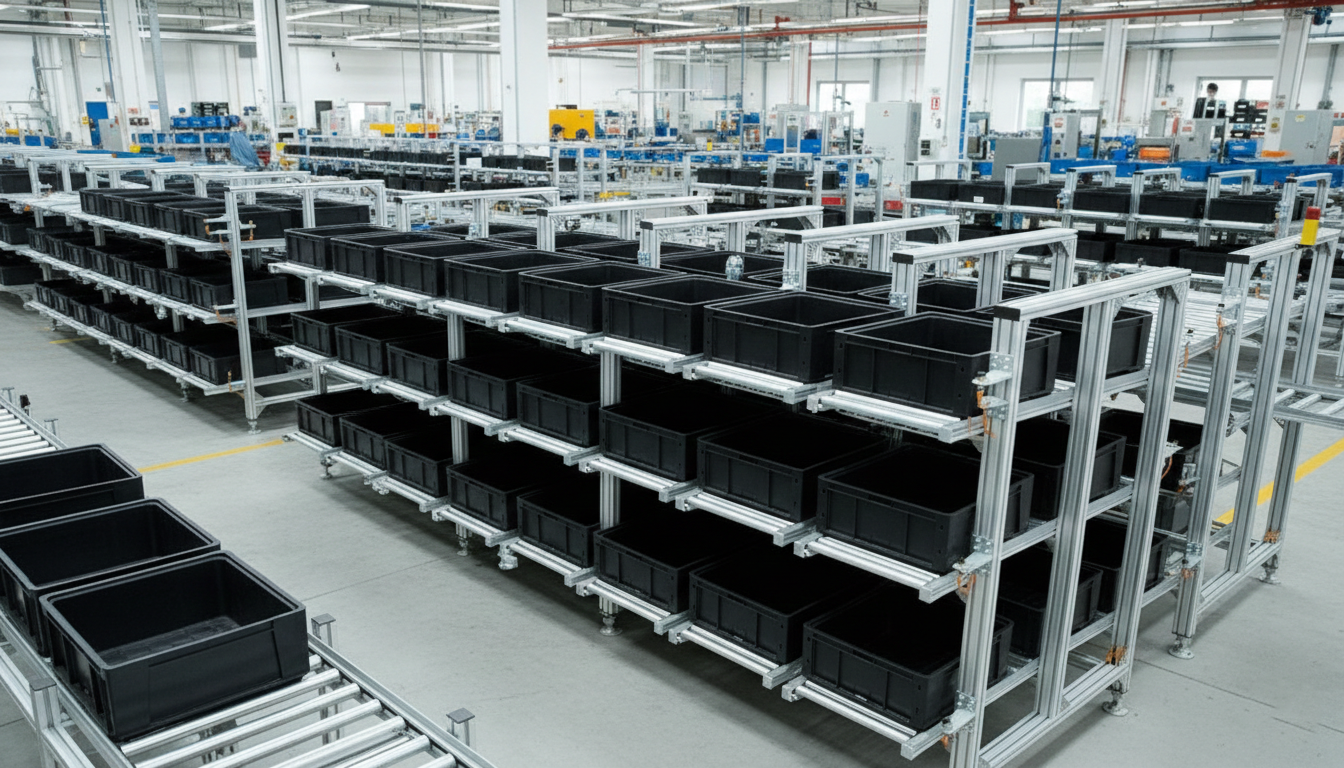
Multi-Level Carton Flow Racks Features
Modular aluminum carton flow rack systems engineered for reliability, flexibility, and lean material flow in any production or distribution environment.
3 to 6 Pick Tiers per Bay
Multi-level frames stack carton flow lanes from floor level to ergonomic reach height — typically 3 tiers for fully ergonomic pick zones, up to 6 tiers when upper levels serve lower-velocity SKUs or are accessed by lift.
Ergonomic Tier Spacing
Tier heights are positioned to minimize operator reach and bend. High-velocity SKUs land at the golden zone (knuckle to shoulder height). Lower-velocity SKUs occupy the lower and upper tiers where occasional reach is acceptable.
Independent Tier Pitch Adjustment
Each tier's lane pitch adjusts independently. Heavier cartons on lower tiers run at lower pitch; lighter cartons on upper tiers may need the same or slightly higher pitch to maintain consistent flow speed.
Vertical Frame Bracing System
Multi-level frames use diagonal bracing and top-tie connections to maintain structural stability at full height under carton load. Frame engineering accounts for live load from all tiers simultaneously at full lane capacity.
Order Pick Cart Integration
Lower tiers align to standing-height pick carts. Upper tier pick levels are integrated into pick module platforms or batch pick lift devices. Cart stop rails and cart alignment guides position the pick cart at each tier interface.
Aisle Label & Pick Light Ready
Multi-level bays include vertical lane numbering columns and tier designation labels for operator navigation. Pick-to-light bracket mounts are integrated into the front frame for each lane position — no retrofitting required.
Technical Specifications
Standard configurations for multi-level carton flow racks systems. Custom lane widths, depths, heights, and track types available for any carton size or facility requirement.
Applications & Industries
Multi-Level Carton Flow Racks systems deliver reliable carton flow performance across a wide range of manufacturing, distribution, and fulfillment environments.
- High-SKU Distribution Centers — 200+ SKU pick bays achieved in a fraction of the floor space of single-level systems. Multi-level density enables zone-based order picking with fewer operator travel steps per order.
- Automotive Assembly Lines — Line-side multi-tier carton racks feed 50+ component SKUs to a single assembly workstation — all within operator arm reach of the workstation without walking.
- Pharmaceutical Fulfillment — Multi-level FIFO carton flow lanes for high-SKU pharmaceutical distribution. Each tier dedicated to a product category for efficient operator batch picking.
- Pick Module Construction — Multi-level carton flow bays are the core pick face element in conveyor-integrated pick modules. Each level discharges to a take-away conveyor belt connecting to order consolidation.
- Food Service Distribution — Dense multi-level pick faces for dry goods, frozen, and refrigerated category pick zones. Cold-rated aluminum and track components for temperature-controlled environments.
- Retail Replenishment DCs — Store replenishment picking from multi-level carton flow bays. Zone-based pick paths visit fewer bays per order with more SKUs available per bay stop.
- E-Commerce Each-Pick Zones — High-velocity product in multi-level pick faces adjacent to each-pick workstations. 3-tier ergonomic configuration keeps all high-velocity SKUs in the picker's primary reach envelope.
- Electronics Component Kitting — Dense component carton lanes for PCB assembly kitting. Multi-level configuration keeps all kit BOM carton sizes within workstation arm reach.
Frequently Asked Questions
Common questions about multi-level carton flow racks specification, configuration, and deployment.
How many tiers can a carton flow rack reach without a lift device?
For fully ergonomic operation without a lift, the maximum is typically 3 tiers with the top tier not exceeding 1800 mm to the lane front face. A 4th tier is accessible with a standard step stool for lower-velocity SKUs. Tiers 5 and 6 require a pick platform, rolling ladder, or pick module mezzanine level to serve.
How is lane pitch set independently for each tier?
Each tier's front and rear frame elevation is set by adjustable frame brackets or by specifying different front and rear frame heights per tier. Pitch adjustment brackets on the track mounting points allow fine-tuning within each tier. Tiers with heavier cartons typically run at 2–4°; lighter cartons at 4–6°.
What is the structural rating for multi-level carton flow racks?
Multi-level frames are engineered for the combined live load of all tiers at full carton capacity, plus a safety factor of 1.5–2.0× per ANSI MH 16.3 racking standards. Frame bracing, post section, and floor anchor sizing are calculated from the actual carton weights and lane depths specified for the project.
Can multi-level racks be extended after initial installation?
Yes. Modular T-slot aluminum frames allow vertical and horizontal extension without replacing the base structure. Adding a tier requires installing new cross beams, lane track, and front/rear panels on the existing posts (if post height accommodates the additional tier). Horizontal extension adds new post-and-beam bays to the row end.
How are upper tier pick faces integrated with pick-to-light systems?
Pick-to-light controllers mount to integrated bracket points in the front frame of each tier. Wiring channels run in the frame vertical cavity to a controller at the base. Each lane's pick-to-light indicator sits at the front edge of the lane at that tier's pick face height, within the operator's sight line for all ergonomic tiers.
What aisle width is needed for multi-level carton flow pick aisles?
Standard pick aisle width for multi-level carton flow racks is 1200–1500 mm for single-sided picking, and 2400–3000 mm for double-sided pick aisles. Aisle width must also accommodate pick cart width and operator passing clearance. Narrower aisles are possible with single-sided bays facing a fixed wall.
Stack More SKUs in Your Pick Aisle
Multi-level carton flow racks engineered for your tier count, carton mix, and ergonomic requirements. Maximum SKU density per aisle foot — built for high-volume, high-SKU operations.
Request a Quote Email Our Team