Pick Module Flow Racks
Carton flow rack bays engineered for integration into multi-level pick modules — with take-away conveyor discharge at each pick level, pick-to-light lane indicators, and frame structures that align to mezzanine floor systems. Designed for high-throughput distribution centers running case-pick, each-pick, or mixed operations.
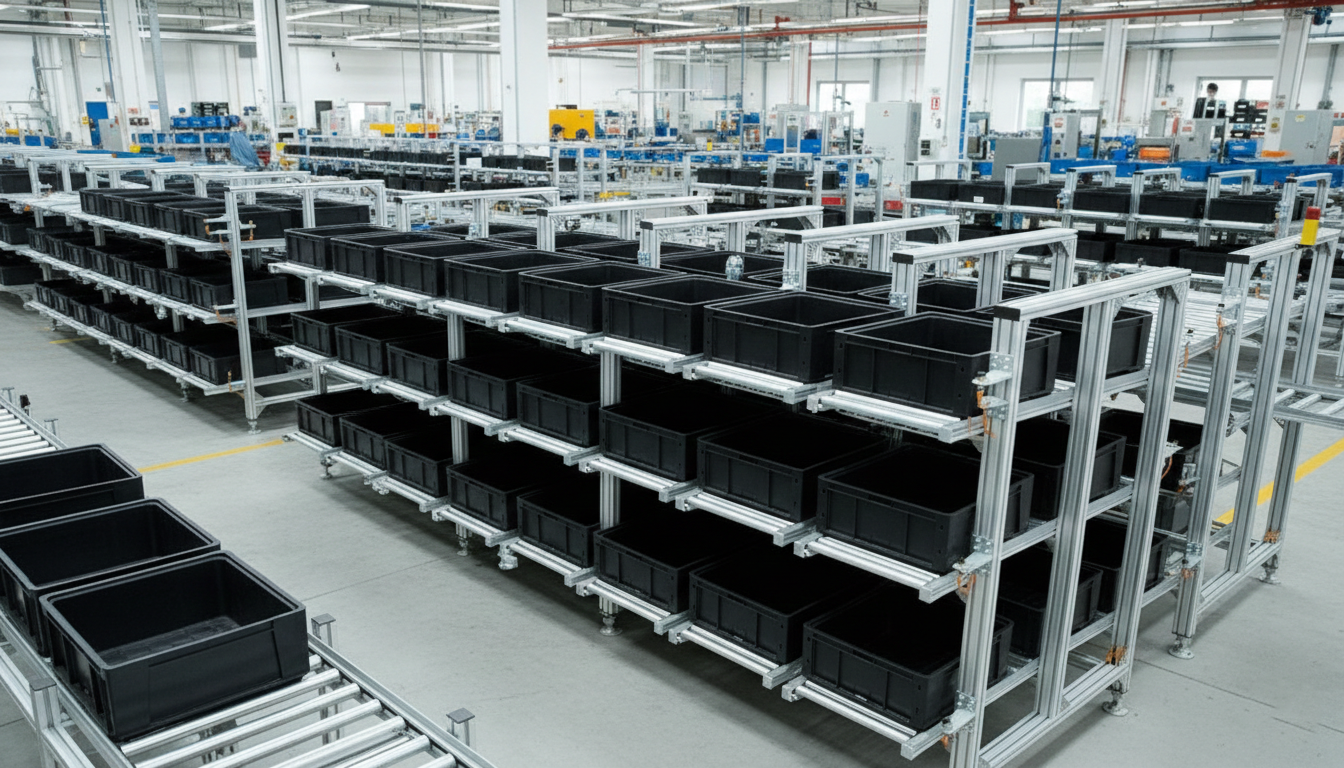
Pick Module Flow Racks Features
Modular aluminum carton flow rack systems engineered for reliability, flexibility, and lean material flow in any production or distribution environment.
Take-Away Conveyor Discharge Integration
Pick module flow rack bays are designed with the take-away conveyor belt running in front of or below the pick face. Cartons or cases are picked directly onto the belt for transport to order consolidation — no tote or cart required for single-level pick module operation.
Multi-Level Mezzanine Alignment
Frame heights and pick face elevations are coordinated with pick module mezzanine floor levels. Each pick level's floor elevation, handrail clearance, and conveyor height are integrated into the rack design package.
Pick-to-Light Integration
Lane-level pick-to-light indicators mount at the front frame of each carton flow lane. Controllers wire through integrated frame conduit channels. Pick-to-light integration with WMS/WCS is a standard deliverable on pick module flow rack projects.
Case and Each-Pick Configurations
Carton flow lanes in pick modules are configured for case-pick (full carton to belt), each-pick (individual units from an open carton), or mixed operations. Each-pick positions include open-face carton presentation with bin rail and unit stop.
Replenishment Aisle Coordination
Replenishment aisle width, forklift or tugger access, and rear-lane load positions are coordinated with the pick module structural layout. Replenishment can occur from the floor level or an upper mezzanine level depending on module configuration.
Fire Suppression & MEP Coordination
Pick module flow rack frame heights and bay layouts are designed with clearance for in-rack sprinkler systems, lighting, and electrical conduit per NFPA 13 and NFPA 230 rack storage standards.
Technical Specifications
Standard configurations for pick module flow racks systems. Custom lane widths, depths, heights, and track types available for any carton size or facility requirement.
Applications & Industries
Pick Module Flow Racks systems deliver reliable carton flow performance across a wide range of manufacturing, distribution, and fulfillment environments.
- Retail Distribution Centers — Case-pick pick modules for store replenishment. Multi-level carton flow bays by product category — ambient, cold, fragile. Conveyor-integrated case flow to sorter and shipping.
- Grocery Wholesale DCs — Dry goods, HBC, and general merchandise pick modules with carton flow replenishment from reserve pallet storage. High-velocity items in lower tiers; medium-velocity in upper levels.
- E-Commerce Fulfillment Centers — Each-pick multi-level pick modules for high-SKU parcel fulfillment. Carton flow lanes present individual unit pick positions at each mezzanine level. Tote conveyors carry picks to consolidation.
- Big Box Retail Replenishment — High-throughput pick modules for full-pallet and case replenishment of large format retail stores. Conveyor-integrated case flow from each-pick levels to pallet build stations.
- Third-Party Logistics (3PL) — Multi-client pick module infrastructure with configurable carton flow bay layouts per client program. Standard frame and conveyor interfaces allow rapid reconfiguration between client transitions.
- Pharmaceutical Distribution — Compliant pick module design for pharmaceutical case picking — each-pick zone with unit serialization scan at pick face; case-pick conveyor for full-case order lines.
- Consumer Goods DCs — Mixed case and each-pick modules for omnichannel consumer goods distribution — same pick module serves B2B case replenishment and B2C parcel picks.
- Automotive Aftermarket DCs — Parts pick modules for dealer replenishment and online retail. High-SKU each-pick levels for small parts; case-pick conveyor levels for bulk consumable lines.
Frequently Asked Questions
Common questions about pick module flow racks specification, configuration, and deployment.
What is a pick module and how do carton flow racks fit into it?
A pick module is a multi-level integrated material handling system combining mezzanine floors, conveyor systems, and storage pick faces. Carton flow rack bays form the pick face storage element at each module level. Cartons are replenished from the rear lane and picked from the front face directly onto a take-away conveyor. The module typically has 2–5 levels, each served by a different product category or velocity tier.
How is pick-to-light integrated into pick module flow rack frames?
Pick-to-light display units mount to integrated bracket positions in the front frame rail of each carton flow lane. Wiring runs through conduit channels in the vertical frame members to a zone controller at the floor level or mezzanine. Controllers interface with the WMS or WCS via Ethernet or dedicated PTL network. Display units, controllers, and wiring are typically furnished by the PTL vendor; Modular Solutions provides the integrated mounting infrastructure.
What fire suppression provisions are required in pick modules?
NFPA 13 and NFPA 230 require in-rack sprinkler systems for high-pile rack storage exceeding 12 feet in height. Pick module carton flow rack frame designs include sprinkler drop clearance at each pick level, horizontal rack sprinkler branch line spacing, and minimum clearance from the top storage position to the ceiling. Local AHJ (Authority Having Jurisdiction) requirements are confirmed during design.
Can pick module carton flow racks be configured for each-pick operations?
Yes. Each-pick positions use open-face carton presentation where the front carton in the lane is opened and units are picked individually. A bin rail at the lane front holds the carton open; a unit stop prevents the carton from sliding forward under pick force. When the front carton is empty, the next carton flows forward. Each-pick and case-pick lanes can be mixed within the same bay.
What is the typical throughput capacity of a pick module carton flow bay?
Pick module throughput depends on the number of lanes, pick rate per operator per hour, and conveyor speed. A single-operator pick position with 60–80 lane positions can achieve 200–400 picks per hour for each-pick operations, or 150–250 case picks per hour. Full pick module throughput is calculated from the number of operator positions, zone balancing, and order wave structure.
How are pick modules expanded when throughput grows?
Modular aluminum frame construction allows pick module bays to be added to existing rows, new rows added to the module aisle, and additional pick levels added by extending post heights or adding mezzanine levels. Conveyor extensions and PTL zone additions are coordinated with the module expansion. Expansion design is included in the original project engineering package.
Engineer Your Pick Module Flow Rack System
Pick module carton flow rack bays designed for your throughput target, SKU profile, conveyor interface, and mezzanine layout. Full engineering package included.
Request a Quote Email Our Team