Gravity flow systems engineered for drums, IBCs, bulk containers, and large material vessels — handling thousands of pounds per lane position while maintaining FIFO rotation for chemical, food, pharmaceutical, and industrial manufacturing operations. Manufactured in Auburn Hills, MI.
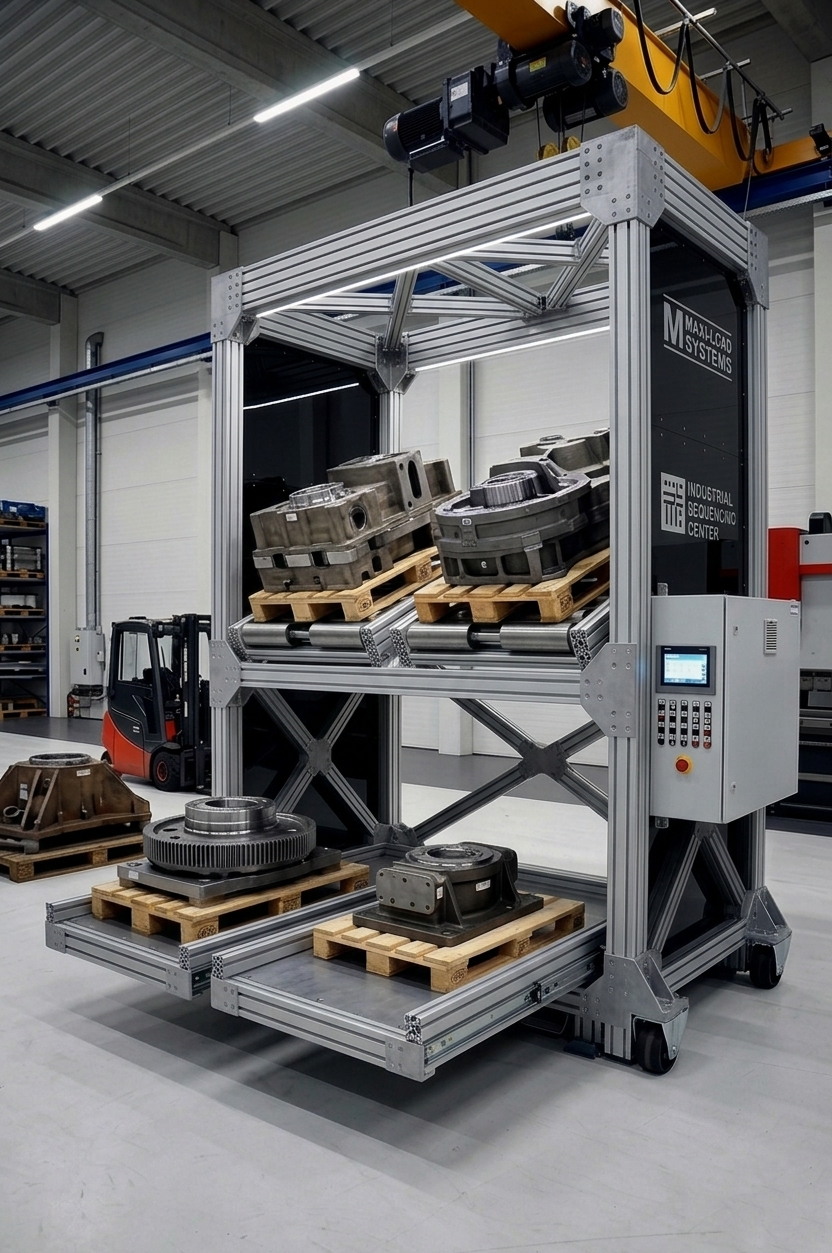
Lane geometry is designed for your specific drum pallet, IBC pallet, or bulk container base — with roller pitch and rail width matched to the container footprint for stable, drift-free gravity flow.
Electrically bonded roller tracks, non-sparking roller materials, and spill containment sump designs are available for flammable liquid drum storage under NFPA 30 and OSHA requirements.
Stainless steel roller tracks, no-crevice design, and FDA-compliant material contact surfaces are available for food, beverage, and pharmaceutical bulk ingredient storage and staging.
Rear-load, front-pick gravity flow enforces FIFO lot rotation for date-coded bulk ingredients, chemicals, and materials — eliminating the risk of older inventory being bypassed for a newer delivery.
Floor-level lane designs allow pallet jack access at the pick face without a forklift — reducing equipment dependency in dispensing areas and simplifying material movement for smaller operations.
Sump trays, drip containment channels, and polyethylene-lined trough structures can be integrated under flow lanes for drum and IBC secondary containment compliance.
55-gal drums on pallets, IBCs on EUR/ISO and GMA pallets, fiber drums, bulk liquid vessels on carriers
Up to 3,500 lbs per position; IBC lanes typically 2,500–3,000 lbs; drum pallet lanes 1,800–2,200 lbs
60–90mm steel; stainless steel option for food/pharma; non-sparking bronze roller available for flammables
3–4% standard; speed controllers per lane; adjusted for drum and IBC container weight
Sump pallet at pick face; under-lane polyethylene trough; containment volume per EPA/OSHA requirement
Continuous electrical bonding through roller track to ground lug for flammable liquid drum lanes
Powder coat standard; galvanized or stainless for corrosive material environments; epoxy for wash-down
2-deep to 5-deep; depth per consumption rate and replenishment frequency
Forklift load aisle; floor-level pallet jack pick face; drum handler pick-face design available
Drum and IBC staging for raw material FIFO lot rotation in chemical blending and processing facilities.
Bulk ingredient IBC and drum lanes with stainless contact surfaces and FIFO lot rotation compliance.
NFPA 30-compliant drum gravity flow lanes with bonded tracks, spill containment, and non-sparking rollers.
FDA-compliant stainless flow lanes for API drum and container staging with lot control and FIFO enforcement.
Drum and pail gravity staging for paint, ink, and coatings dispensing with spill containment integration.
Pesticide and herbicide drum staging lanes with secondary containment for EPA compliance.
Oil, lubricant, and coolant drum staging in gravity lanes for automotive and industrial manufacturing dispensing.
Bulk flavor, concentrate, and additive IBC staging lanes at blending and filling operations.
Bulk material gravity flow systems can handle 55-gallon steel and poly drums on pallets, IBCs (intermediate bulk containers) on EUR/ISO or GMA pallets, fiber drums, metal drums, bag-in-box bulk liquid containers, and custom bulk vessel carriers. The flow rack is designed for the container base or pallet type, not the vessel itself.
Yes, with appropriate design considerations. Flow racks for hazardous material drums require spill containment trays or sump pallets at the pick face, electrically bonded roller tracks for flammable liquid drums, and non-sparking roller materials where required by NFPA 30 or local fire code. Modular Solutions can design to specific NFPA, OSHA, or customer safety standards for flammable, combustible, and corrosive material storage.
Full drums are loaded at the rear of the lane on their pallet using a forklift or pallet jack. The drum-plus-pallet gravity feeds forward on the lane rollers. At the pick face, a pallet jack or drum handler removes the front pallet for dispensing or use. A forklift is not required at the pick face if the lane is designed for floor-level pallet jack access. Safety pallet stops retain the front pallet until deliberately removed.
Yes. Food and pharmaceutical applications require stainless steel roller tracks, no-paint contact surfaces, and designs that eliminate crevices where product or cleaning residue can accumulate. Modular Solutions can specify FDA-compliant materials and design flow lanes that meet FSMA, GMP, and NSF standards for food and pharmaceutical bulk material handling.
A full IBC on a pallet can weigh 2,500–3,000 lbs. A pallet of 4 x 55-gallon drums fully loaded weighs approximately 1,800–2,200 lbs. Lane ratings are calculated from the specific container and content weight, with roller, rail, and frame members sized to carry the maximum lane load (all positions full) with a 2:1 safety factor.
Tell us your container type, content weight, lane count, and any hazmat or regulatory requirements — our engineers will design a compliant, safe system for your operation.
Request a Quote